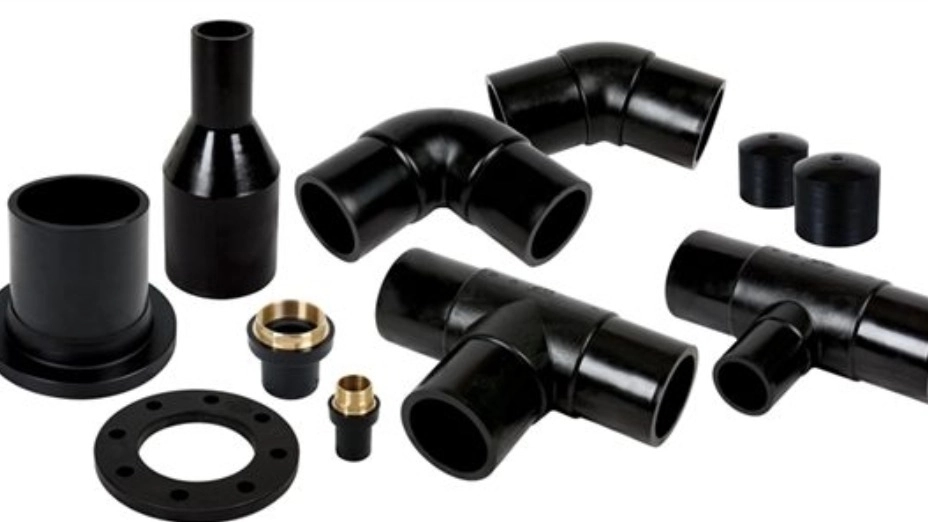
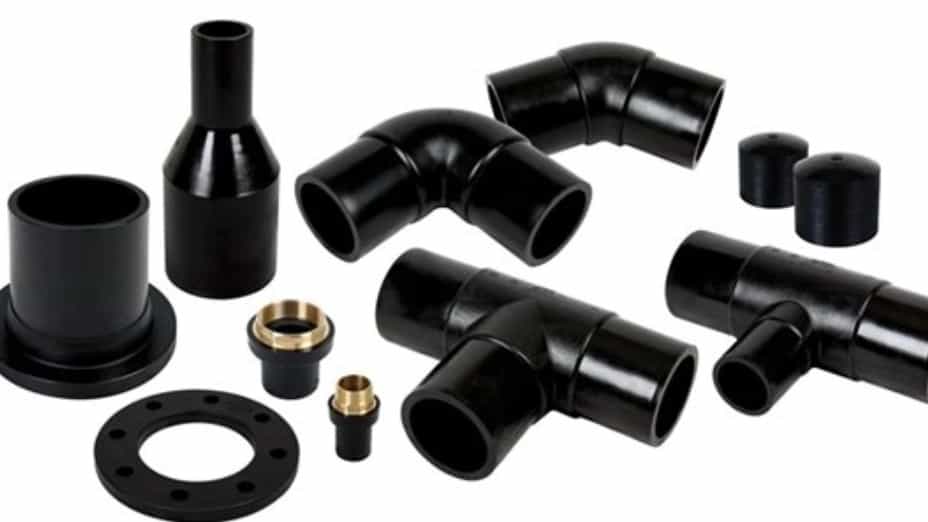
Welded joints, to install them to the pipe, a welding machine must be used. Welded joints are produced in four general pressure categories: 4 bar, 6 bar, 10 bar and 16 bar (atmosphere)
Introducing and applying polyethylene joints
All manufactured polyethylene welding connections that have a standard and are supposed to be used in irrigation or water supply projects must have the following minimum features:
Proper resistance against breakage and cracking caused by external pressures on them Resistance to chemicals such as agricultural fertilizers Resistance to corrosion, abrasion and vibrations caused by earthquakes Being resistant to rust Smooth and polished internal and external walls, no sedimentation and very low pressure drop due to internal surface friction
Polyethylene fittings
Urban water supply pipelines Agricultural water transfer Use in drip irrigation and rain irrigation networks City gas transfer and so on. Welded polyethylene joints are of very high quality and if grade A polyethylene PE100 materials are used in its production process and if the manufacturing plant has an equipped laboratory and a quality control unit.
Polyethylene welding process process
During the welding process with the polyethylene pipe welding machine, we must pay attention to important things. The thickness of the pipe that we want to weld to one of the connections must be the same. For example, if the pipe has a pressure of 10 bar, we must use connections with a pressure of 10 bar, and their thickness is the same. Due to the fact that this pipe and fittings are black in color and attract dust, we must clean and dust the welding area with a soft tissue before welding and adjust their edges. To perform an application for welding, welding pressure and parameters of temperature and welding time must be carefully adjusted. Before starting welding, the temperature of the welding machine must be fully controlled, which is done by an infrared thermometer. The heating plate should be removed at least 15 minutes after reaching the temperature. To ensure good welding quality, the heating plate should be cleaned with soft cleaning materials using alcohol, etc. before welding. The heater plates (Teflon) must be undamaged.